How to choose roller return conveyor and belt return conveyor for edge banding machine?
Roller Return Conveyor Line
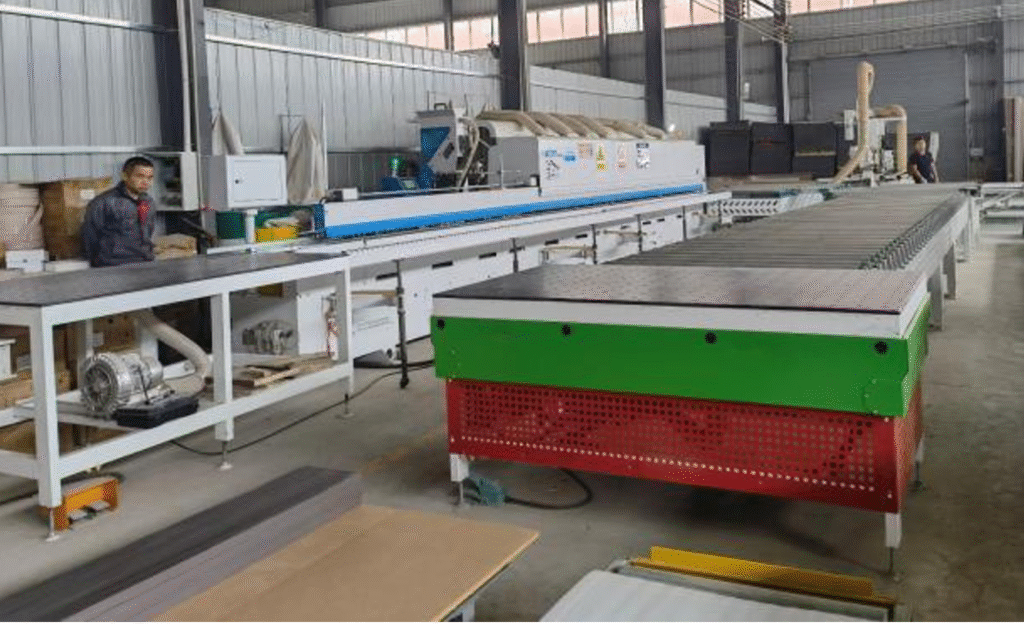
This system features segmented support using multiple rubber-coated rollers, point-contact rolling conveyance, and independent roller drives. Directional changes are achieved via a pneumatic lifting platform that raises the load onto a belt-based transfer bridge; the load is then lowered back onto the rollers for the return run. Roller return conveyor utilizes a segmented, modular structure.
Belt Return Conveyor
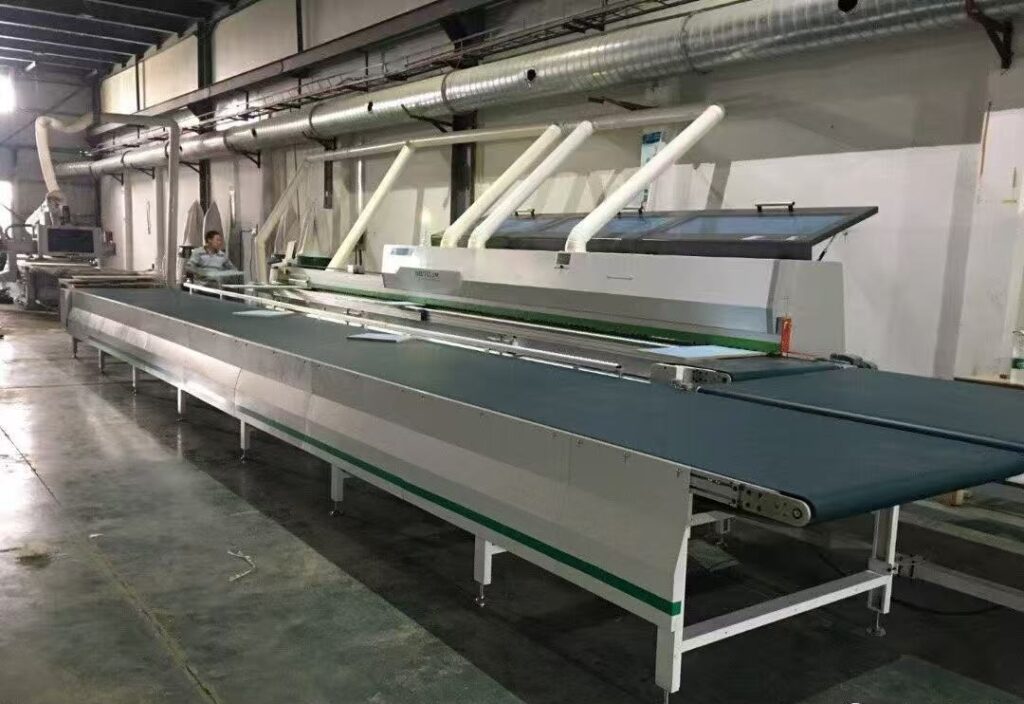
The system features a continuous PVC/PE loop belt that fully covers the surface and runs over a flat, flexible support bed, driven by the overall friction between the belt and the pallets. A single, continuous belt handles transport across both straight and curved sections, while a pneumatic cylinder-actuated lifting mechanism raises the belt to facilitate pallet transfer and recirculation.
1. Panel Compatibility and Surface Protection
**Blet Return conveyor**
✅ **Advantages:**
• Full-surface contact ensures stability; tiny panels, narrow strips, and irregularly shaped thin panels do not tilt or fall off (handles panels as narrow as 60mm).
• No roller pressure marks on high-gloss, PET, or soft-touch panels; leaves no traces and offers superior surface protection.
• No slipping during turns or inclines; small workpieces do not tip over.
❌ **Disadvantages:**
• Sawdust and adhesive powder stick to the belt; long-term dust accumulation causes slipping and tracking issues, potentially marking the panel surface.
• Poor load-bearing capacity for heavy doors or large panels; large panels may sag or deform in the center.
**Roller-Type Return Conveyor**
✅ **Advantages:**
• Exceptional load-bearing capacity; suitable for 18–40mm thick door panels and large sheets without deformation under heavy loads.
• Sawdust falls through roller gaps, preventing dirt buildup; easy to clean and rarely slips.
• Point contact minimizes the risk of large-area surface scratches caused by dust.
❌ **Disadvantages:**
• Narrow or small panels may get stuck in roller gaps, drift off-track, or fall.
• Prolonged heavy pressure can leave uniform roller indentations; use with caution for high-gloss panels.
2. Stability and Conveying Precision
**Belt-Type Return Conveyor**
• Smooth operation at low speeds; synchronizes well with edgebander infeed, ensuring accurate positioning for small parts.
• Drawbacks: Belts tend to stretch and drift in high-temperature, dusty environments, requiring frequent tracking adjustments; large panels may vibrate at high speeds.
**Roller-Type Return Conveyor**
• High mechanical rigidity; stable without wobbling during high-speed, heavy-load transport; maintains precision during continuous, long-term production.
• Segmented drive system; a fault in one section does not affect the entire line; mature accumulation/buffering function allows for temporary panel storage.
3. Maintenance, Lifespan, and Consumables
**Belt-Type Return Conveyor**
• Lower initial purchase cost; simple structure.
• High consumable costs: belts require replacement every 6–12 months; tracking and tensioning rollers need regular adjustment; belt cleaning is time-consuming.
• Dust and hot-melt adhesive degrade the belt, leading to rapid aging.
**Roller-Type Return Conveyor**
• Higher overall machine cost; involves numerous components such as motors and rollers.
• Long service life: Rubber-coated rollers need replacement every 2–3 years, while the metal frame is virtually maintenance-free; wood chips fall away automatically, making daily cleaning simple.
• Low failure rate; suitable for continuous, round-the-clock mass production.
4. Space and Layout Flexibility
Belt-type return line
• Easier to configure turns and inclines; compact U-shape design; ideal for smaller workshops.
• Integrated, unitary structure; extending or modifying the line later is difficult.
Roller-type return line
• Modular assembly; easily extended or adjusted (adding/removing workstations); integrates well with panel saws or six-sided drilling lines.
• Complex turning mechanisms; requires a wider footprint; unsuitable for very cramped workshops.
5. Speed and Production Capacity
• Belt type: 0–35 m/min; highly efficient for batch processing small parts; rapid circulation of individual small panels.
• Roller type: 0–30 m/min; clear advantages for continuous mass production of large panels and thick doors; buffering capability prevents material jams.
6. Recommended Workshop Scenarios
Choose the belt-based return line if:
1. You operate a small “whole-house customization” factory with limited floor space.
2. You primarily process small cabinet panels, narrow strips, thin back panels, or small irregular parts.
3. You process high-gloss, soft-touch, or matte finishes and need to avoid roller pressure marks.
4. Daily output is under 500 panels and the budget is limited.
Choose the roller-based return line if:
1. You operate a medium-to-large factory or a wooden door plant that regularly handles large panels and thick door slabs.
2. Daily output exceeds 1,000 panels with continuous two- or three-shift operations.
3. The environment is dusty or involves heavy use of PUR edge-banding adhesive, and you want to minimize frequent equipment cleaning.
4. You need to integrate with automated production lines or link multiple machines together.